- ISO 9001:2015 Certified Company
Chemical Storage Tanks in India
Top Chemical Storage Tank Manufacturers in India 2026
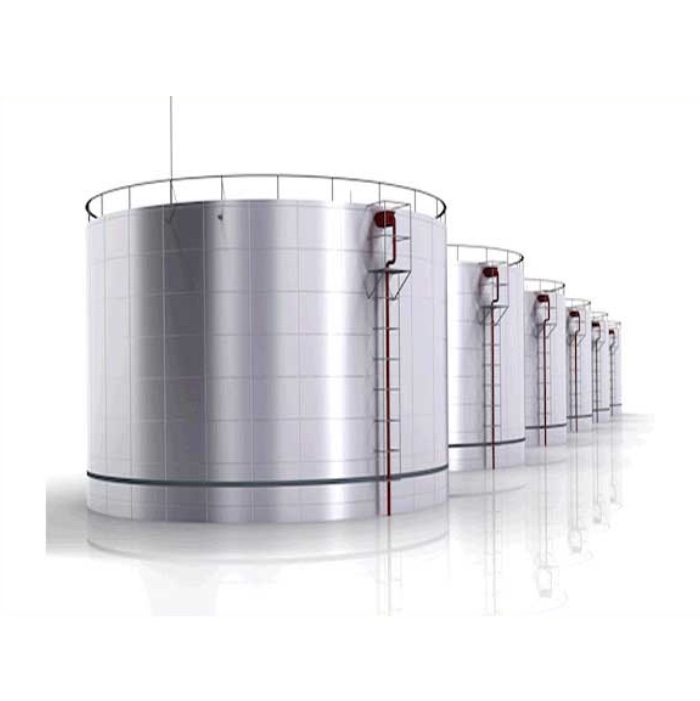
Suyom Engineering is a genuine Chemical Storage Tanks Manufacturers in India, Suppliers and Exporters in India, founded in 2018; we have established ourselves as a trusted name in designing and manufacturing high-performance industrial machinery. We utilize quality-checked materials and advanced manufacturing capabilities to deliver precise, reliable, durable, and low-maintenance solutions. Guided by our tagline, “Engineering for Excellence,” we provide engineered solutions that help customers achieve their operational objectives while delivering engineered storage solutions for corrosive, reactive, hazardous, and process chemicals across diverse industrial environments. Our Chemical Storage Tanks combine material compatibility, structural integrity, controlled fabrication, leak prevention, and modern monitoring provisions to support reliable chemical handling.
Chemical Storage Tanks Suppliers and Exporters in India
Our Chemical Storage Tanks are also supplied and supported across major industrial areas in India, including Pune, Mumbai, Ahmedabad, Vadodara, Surat, Hyderabad, Chennai, Bengaluru, Delhi-NCR, and Gujarat’s key chemical manufacturing hubs. Our presence across these industrial regions enables us to serve chemical, pharmaceutical, agrochemical, specialty chemical, and process industries with durable, corrosion-resistant, and application-specific storage solutions designed for safe and reliable chemical handling.
What Is a Chemical Storage Tank and Why Is It Used?
A Chemical Storage Tank is an engineered Chemical Storage Vessel designed to safely contain acids, alkalis, solvents, process chemicals, and other industrial liquids without compromising product integrity. Unlike a conventional Water Tank or water Storage Tank, chemical vessels require carefully selected materials, liners, fittings, and construction methods according to chemical concentration, temperature, density, and operating conditions. In 2026, advanced tank designs increasingly incorporate corrosion-resistant construction, level sensing, secondary containment, and condition-monitoring provisions for safer and more traceable storage.
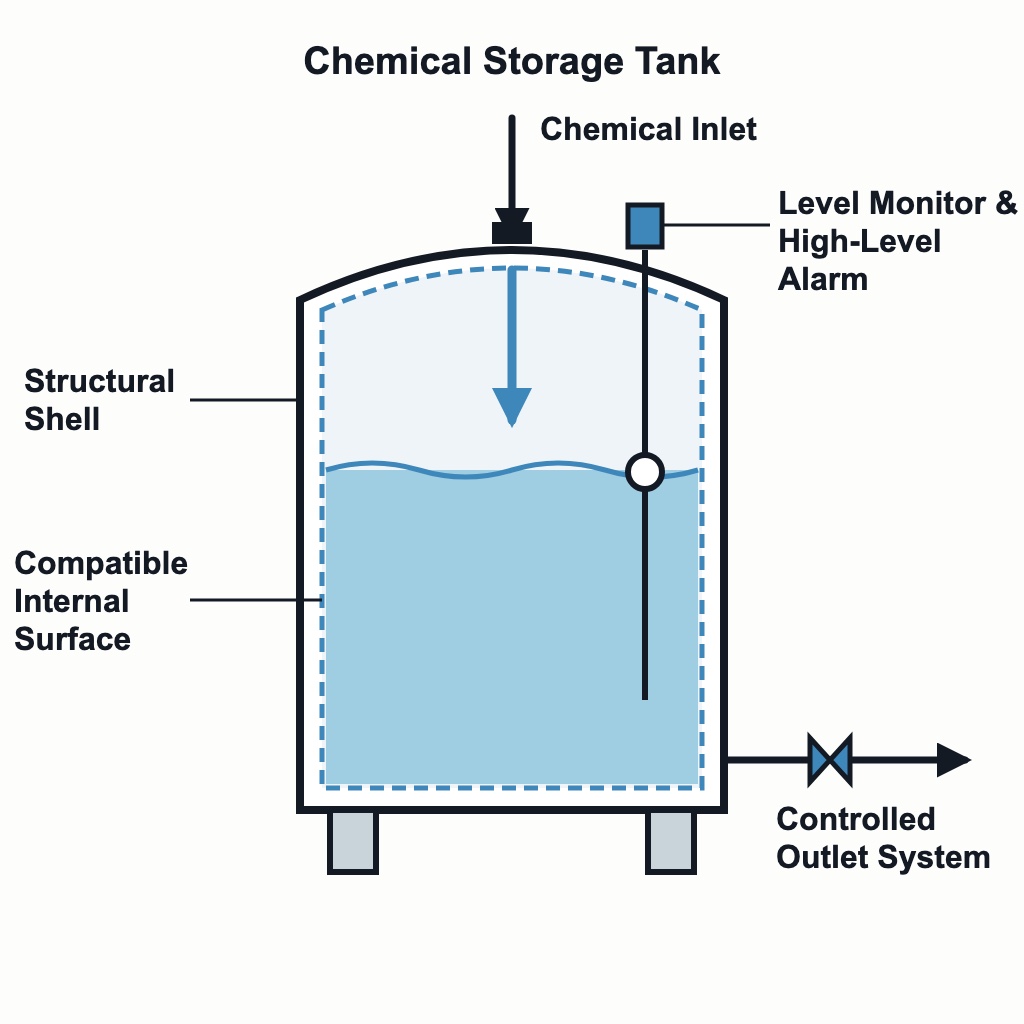
How Does a Chemical Storage Tank Work?
- Chemical Inlet: Appropriately sized inlet connections enable safe and efficient chemical filling.
- Structural Shell: Robust construction withstands the pressure, weight, and properties of the stored chemical.
- Compatible Internal Surfaces: Chemical-resistant materials help prevent corrosion, contamination, and premature tank deterioration.
- Controlled Outlet System: Valves, outlets, and transfer systems ensure controlled and secure chemical dispensing.
- Modern Instrumentation: Digital level monitoring and high-level alarms provide enhanced visibility and help prevent overfilling.
Types of Chemical Storage Tanks We Manufacture
A well-known Chemical Storage Tanks manufacturers in India, we are providing the best quality Chemical Storage Tanks such as:
- Fiberglass Tanks (FRP): Fiberglass Tanks (FRP) provide strong corrosion resistance with comparatively low maintenance requirements for acids, alkalis, and process liquids. We engineer FRP Tank construction according to chemical compatibility, capacity, temperature, and mechanical loading requirements. Advanced resin systems, improved laminate designs, and inspection-controlled fabrication make them suitable for modern chemical-processing environments.
- Polyethylene Tank: Polyethylene Tank solutions offer corrosion resistance and practical handling for compatible chemicals used in treatment and processing facilities. We select suitable polyethylene grades and wall construction according to chemical concentration, operating temperature, and service conditions. Modern rotational-moulding and fabrication practices help provide seamless, durable storage for selected industrial applications.
- Stainless Steel Chemical Storage Vessel: Stainless Steel construction provides mechanical strength, hygienic surfaces, and resistance to many chemical environments when the correct alloy is selected. We consider concentration, temperature, chloride exposure, and process conditions before specifying stainless-steel construction. Automated fabrication, controlled welding, and improved surface-finishing practices support reliable service in demanding applications.
- Steel Storage Tank: Steel Storage Tank designs provide high structural strength for large-capacity Industrial Storage Tank requirements where robust mechanical construction is essential. We can integrate suitable internal coatings or linings when the stored chemical requires additional corrosion protection. Modern fabrication inspection and dimensional quality controls help improve durability, safety, and installation consistency.
Technical Specifications
| Parameter | Specification |
|---|---|
| Tank Material | SS 304 / SS 316 / PP / HDPE / FRP |
| Storage Capacity | 500 to 100,000+ Litres |
| Tank Type | Vertical / Horizontal / Atmospheric |
| Design Pressure | Atmospheric to customized pressure rating |
| Operating Temperature | Up to 150°C, application dependent |
| Tank Thickness | Typically 3–20 mm, as per design |
| Surface Finish | Pickled, Passivated or Mirror Finish |
| Nozzle Size | Customized as per process requirement |
| Accessories | Manhole, Vent, Level Indicator, Drain & Overflow |

Which Features Make Chemical Storage Tanks Safer and More Efficient?
One of the leading Chemical Storage Tanks Suppliers in India, our all-types of Chemical Storage Tanks is included with new technological formulations such as:
- Corrosion-Resistant Material Selection: We match construction materials, coatings, liners, and resins with the chemical characteristics to minimise premature degradation. This approach can support longer service life than using generic storage materials. Material compatibility evaluation remains essential for modern chemical storage.
- Advanced Leak and Level Monitoring: We can accommodate level sensors, high-level alarms, leak detection, and monitoring interfaces for improved operational control. These technologies help operators identify abnormal conditions before they develop into larger handling problems. Digital monitoring is increasingly valuable for connected industrial facilities in 2026.
- Reinforced Structural Construction: We design shell thickness, reinforcement, supports, nozzles, and mounting arrangements according to application-specific mechanical requirements. This helps the tank withstand operational loads and installation conditions. Improved engineering analysis and fabrication controls support consistent structural performance.
Where Are Chemical Storage Tanks Commonly Used?
Being the best Chemical Storage Tanks Exporters in India, our all types of Chemical Storage Tanks are included with new feature and highly used in multiple applications such as:
- Chemical Processing Plants: We provide storage solutions for acids, alkalis, solvents, intermediates, and process chemicals used throughout chemical manufacturing. Compatible materials and appropriate fittings help maintain safe chemical containment. Advanced monitoring can support process inventory management.
- Water and Wastewater Treatment: Our tanks can store treatment chemicals such as dosing solutions, neutralising agents, and other compatible process liquids. This complements specialised Water Tank and water Storage Tank requirements within treatment facilities. Level monitoring and controlled transfer provisions can improve dosing-system reliability.
- Pharmaceutical and Food Processing: We supply suitable storage configurations for compatible process liquids where material selection, cleanliness, and controlled handling are important. Stainless Steel systems can support applications requiring hygienic and cleanable surfaces, including certain eatable oil storage tank environments. Application-specific material validation remains necessary before selecting the final construction.
- Oil, Petrochemical and Energy Facilities: Our storage systems can be engineered for compatible oils, additives, treatment chemicals, and process liquids used in energy-related operations. Where appropriate, specialised designs complement an Oil Storage Tank or broader industrial containment system. Safety accessories and monitoring provisions can improve operational control.
How Do Chemical Storage Tanks Support Today's Industrial Market?
| Industrial Requirement | Our Storage Advantage |
|---|---|
| Corrosive chemical handling | Compatible FRP, polyethylene, stainless steel, and lined construction helps resist chemical attack. |
| Higher process visibility | Digital level monitoring and alarm integration can improve inventory and operational awareness. |
| Large-volume storage | Engineered Industrial Storage Tank configurations support scalable chemical inventories. |
| Safer plant operations | Leak detection, suitable vents, controlled outlets, and secondary containment provisions can reduce operational risks. |
| Sustainability goals | Durable materials, longer service intervals, and efficient monitoring can support resource-conscious plant management. |
How We Manufacture Chemical Storage Tanks for Modern Industries?
- Application-Suitable Materials: FRP composites, polyethylene, carbon steel, stainless steel, and specialised liners or coatings are selected according to chemical compatibility and service conditions.
- Engineering & Material Selection: Each tank is engineered based on capacity, chemical properties, mechanical requirements, operating conditions, and intended application.
- Advanced Fabrication: Cutting or moulding, fabrication, reinforcement, lining, and finishing are performed using modern manufacturing practices.
- Nozzle & Fitting Installation: Precisely positioned nozzles, fittings, connections, and accessories are integrated to meet process and operational requirements.
- Quality & Inspection: Dimensional inspection, application-specific quality checks, and modern monitoring provisions help ensure reliable and market-relevant storage systems.
Why Choose Us as a Chemical Storage Tanks Manufacturers in India?
- Industrial Core Expertise & Experience: Founded in 2018, Suyom Engineering brings years of experience in industrial machinery and chemical storage solutions, backed by application-focused engineering expertise.
- Application-Specific Engineering: We design Chemical Storage Tanks according to chemical compatibility, capacity, temperature, structural requirements, and specific operating conditions.
- Quality-Checked Materials: We use carefully selected FRP, HDPE, PP, stainless steel, carbon steel, and compatible liners or coatings to support reliable long-term performance.
- Advanced Manufacturing & Quality Control: Modern fabrication practices, controlled welding, reinforcement, finishing, dimensional inspection, and application-specific quality checks help ensure consistent tank performance.
- Reliable & Future-Ready Solutions: Our tanks can incorporate level monitoring, high-level alarms, leak detection, and other modern provisions to support safer, efficient, and traceable chemical storage.
Suyom Engineering is a genuine Chemical Storage Tanks Manufacturers in India, Suppliers and Exporters in India. We delivers engineered Chemical Storage Tanks designed around chemical compatibility, structural reliability, operational safety, and evolving industrial requirements. Our material options, modern fabrication practices, monitoring provisions, and application-focused engineering help industries select dependable storage solutions for present and emerging chemical-handling needs. Contact us today for more information!
Frequently Asked Questions (FAQs)
The best material depends on the chemical, concentration, temperature, capacity, and operating environment, with FRP, polyethylene, stainless steel, and steel serving different applications.
We determine capacity according to chemical inventory, process requirements, available installation space, operating volume, and required safety allowance.
Yes, appropriately engineered FRP, polyethylene, stainless steel, or lined tanks can store compatible corrosive chemicals after material compatibility evaluation.
Yes, tanks can be equipped with level sensors, high-level alarms, leak detection, and compatible digital monitoring systems.
Yes, they can be engineered for chemical processing, water treatment, pharmaceuticals, manufacturing, petrochemicals, utilities, and other compatible industrial applications.