- ISO 9001:2015 Certified Company
Chemical Reactors in India
Top Chemical Reactor Manufacturers in India 2026
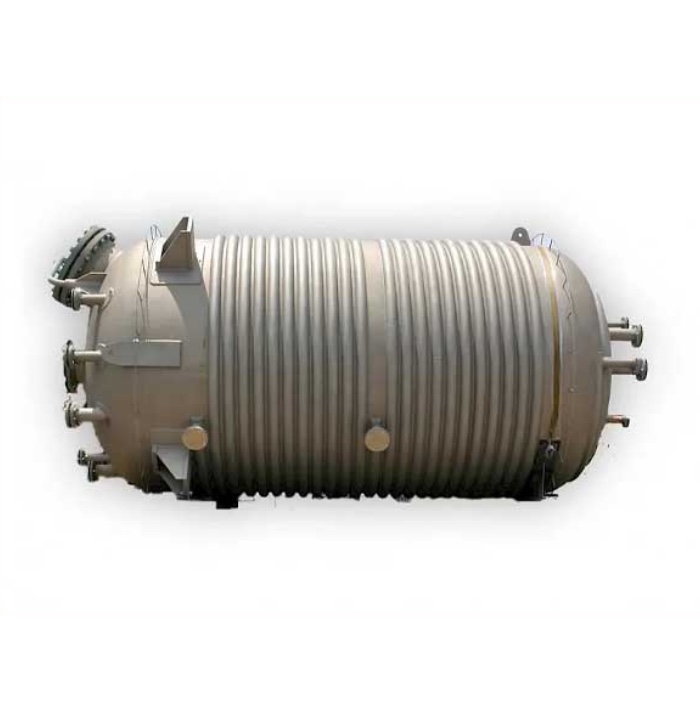
Suyom Engineering is a leading Chemical Reactor Manufacturers in India, Suppliers and Exporters in India, Founded in 2018; we have established ourselves as a trusted name in the design and manufacturing of high-performance industrial machinery. We use quality-checked materials and advanced manufacturing capabilities to provide precise, reliable, durable, and low-maintenance solutions. Guided by our tagline, “Engineering for Excellence,” we deliver engineered solutions that help our customers accomplish their operational goals.
We deliver engineered reaction vessels for controlled chemical processing, effective heat transfer, safe mixing, and consistent production. Our reactor systems are developed around process chemistry, operating temperature, pressure, material compatibility, agitation requirements, and production capacity, with modern automation increasingly enabling precise and repeatable operation.
Chemical Reactor Suppliers and Exporters in India
With a strong presence across India’s major industrial areas, we supply and support our Chemical Reactors for diverse chemical processing requirements in key hubs such as Mumbai, Pune, Ahmedabad, Vadodara, Surat, Hyderabad, Chennai, Bengaluru, Delhi-NCR, and Ankleshwar. Our reach across these industrial centres enables us to serve customers requiring reliable reaction vessels, efficient heat transfer, controlled mixing, and automation-ready process solutions.
What Is a Chemical Reactor and How Does It Work?
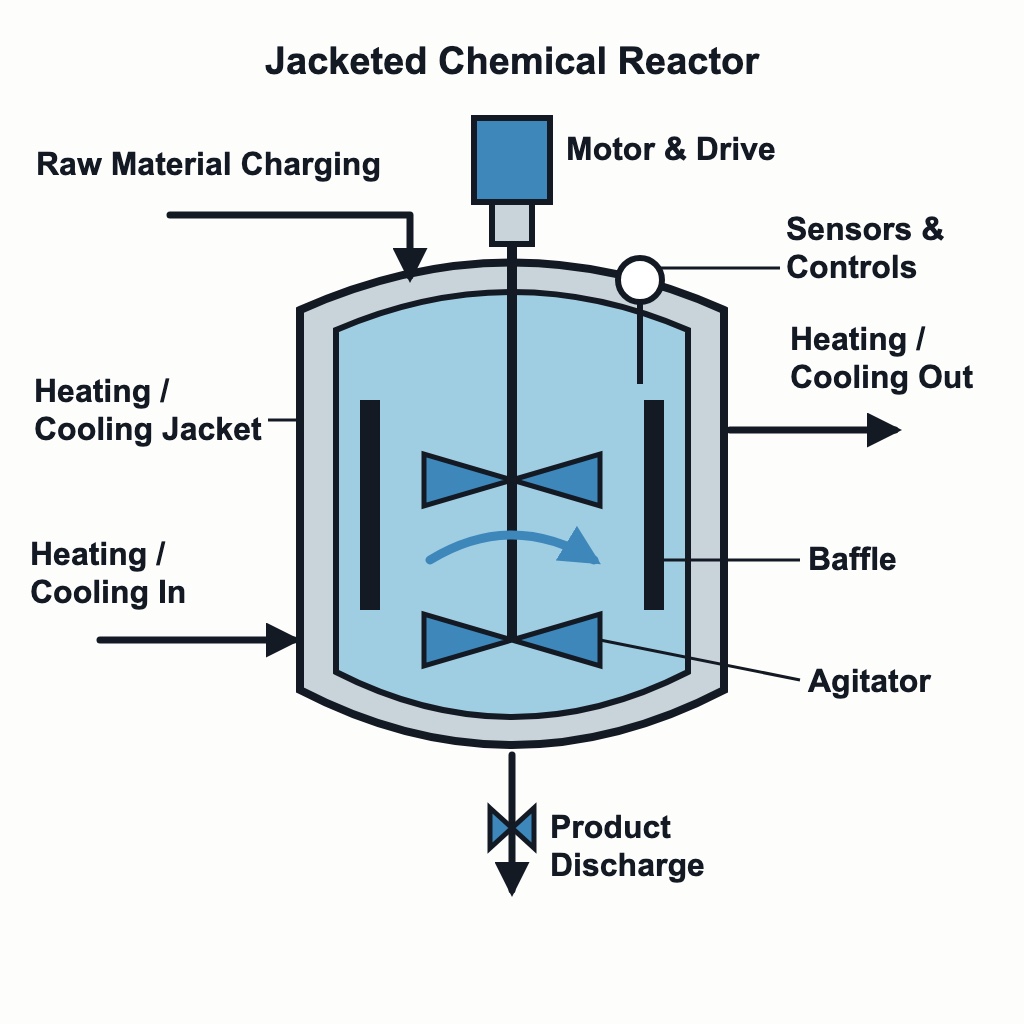
- Controlled Reaction Environment: Provides precise control of temperature, pressure, mixing, and reaction time for consistent chemical processing.
- Efficient Heat Transfer: Uses jackets, coils, or other heating and cooling systems to maintain the required reaction temperature.
- Effective Mixing: Agitators and baffles ensure uniform blending, heat distribution, and mass transfer throughout the reaction.
- Process Monitoring & Automation: Integrated sensors, valves, and control systems enable accurate monitoring and automated regulation of critical parameters.
- Safe Product Processing: Supports controlled raw-material charging, optimized reaction conditions, and safe product discharge after the required conversion is achieved.
Types of Chemical Reactor we offer
A well-known Chemical Reactor manufacturers in India, we are providing the best quality Chemical Reactor such as:
- Stainless Steel Chemical Reactor: We manufacture stainless steel reactors for corrosive and demanding chemical processes requiring hygienic and durable construction. Grades such as SS 304 and SS 316/316L can be selected according to chemical compatibility and operating conditions. Advanced instrumentation and automated temperature control can improve reaction consistency and process monitoring.
- Jacketed Batch Reactor: Our jacketed batch reactors provide controlled heating and cooling around the reaction vessel for flexible production. They are suitable for formulations where ingredients must be charged, reacted, sampled, and discharged batch by batch. Automated sensors and programmable controls can support repeatable temperature profiles and improved energy management.
- 3kL Chemical Reactor: Our 3kL Chemical Reactor configuration supports medium-scale industrial production where controlled mixing and thermal management are essential. We can engineer the vessel with suitable agitators, baffles, jackets, nozzles, and instrumentation according to process requirements. Such scalable Industrial Reactor designs can support efficient transition from laboratory or pilot production toward commercial manufacturing.
Technical Specifications
| Specification | Technical Details |
|---|---|
| Reactor Type | Batch, stirred, pressure, or customized reactor |
| Capacity | 100–50,000 Litres |
| Material of Construction | SS 304, SS 316/316L, or alloy steel |
| Operating Temperature | Up to 300°C, based on design |
| Operating Pressure | Vacuum to 10 bar or as required |
| Agitator Type | Anchor, paddle, turbine, or propeller |
| Heating/Cooling | Jacket, half-pipe coil, or internal coil |
| Surface Finish | Pickled, passivated, or polished |
| Nozzle Configuration | Customized as per process requirements |

What Features Make Our Chemical Reactors Efficient?
One of the leading Chemical Reactor Suppliers in India, our all-types of Chemical Reactor is included with new technological formulations such as:
- Precision Agitation and Mixing: Our reactors can use appropriately selected agitator geometries to achieve uniform blending and effective mass transfer. Baffles and variable-speed drives can be incorporated where the process requires improved mixing performance. Digital monitoring of rotational speed and process conditions can further improve operational control.
- Advanced Thermal Management: We design jackets, coils, and heat-transfer arrangements according to reaction temperature and thermal load. Controlled heating and cooling help maintain stable reaction conditions while reducing unwanted temperature fluctuations. Modern sensors and automated control loops support accurate thermal regulation during demanding production cycles.
- Process Monitoring and Automation: Our reactor systems can accommodate temperature, pressure, level, pH, and other process sensors according to application needs. Automated control architecture enables operators to monitor critical parameters and maintain predefined operating conditions. In 2026, digital twins and AI-assisted optimisation are emerging as important technologies for predictive monitoring and process improvement.
Where Are Chemical Reactors Used?
Being the best Chemical Reactor Exporters in India, our all types of Chemical Reactor are included with new feature and highly used in multiple applications such as:
- Pharmaceutical Manufacturing: Our reactors support synthesis, formulation, crystallisation, and other controlled pharmaceutical processes. Accurate agitation and temperature regulation help maintain batch consistency. Automated monitoring can support improved process repeatability and documentation.
- Specialty and Fine Chemicals: Our reaction vessels are suitable for producing intermediates, additives, solvents, resins, and specialty formulations. Material selection and process-specific design help manage corrosive or temperature-sensitive chemistry. Advanced flow and reaction modelling can assist process optimisation and scale-up.
- Agrochemical Production: Our Industrial Reactor systems support controlled reactions used for agrochemical intermediates and formulations. Efficient mixing and heat removal can help maintain stable reaction conditions. Instrumentation can provide closer monitoring of temperature, pressure, and other critical variables.
- Polymers, Resins and Adhesives: Our reactors facilitate polymerisation, condensation, blending, and formulation processes requiring controlled thermal and mechanical conditions. Variable-speed agitation can accommodate changing viscosity during production. Suitable vessel metallurgy and heating arrangements can improve operational reliability.
- Chemical and Process Industries: Our reactors can be configured for general-purpose chemical synthesis, neutralisation, esterification, hydrogenation, and other industrial reactions. Flexible vessel configurations allow adaptation to different production requirements. This supports current market demand for safer, scalable, energy-conscious, and digitally monitored processing.
Industrial Benefits and Current Market Relevance
| Industrial Requirement | How Our Chemical Reactor Helps |
|---|---|
| Production scalability | Configurable capacities support pilot-to-commercial process expansion. |
| Process consistency | Controlled mixing, temperature, pressure, and residence time improve repeatability. |
| Energy efficiency | Optimised heat-transfer systems can reduce unnecessary heating and cooling demand. |
| Smart manufacturing | Sensors, automation, data acquisition, and digital monitoring support Industry 4.0 operations. |
| Process safety | Controlled operating parameters and monitoring help identify abnormal conditions earlier. |
Manufacturing Process
- Process Requirement Analysis: We assess capacity, operating conditions, chemical properties, temperature, pressure, and application requirements.
- Material Selection & Engineering: We select suitable stainless steel or process-compatible materials and prepare precise engineering drawings.
- Precision Fabrication: We perform accurate cutting, forming, welding, nozzle integration, and jacket or coil fabrication.
- Surface Finishing & Inspection: We complete required surface finishing followed by dimensional and fabrication quality inspections.
- Testing & Final Dispatch: We conduct appropriate pressure and quality checks to ensure reliable performance before final dispatch.
Why Choose Us as a Chemical Reactor Manufacturers in India?
- Industry Experience & Engineering Expertise: With years of experience since our founding in 2018, we combine industrial core expertise with process-focused reactor engineering for diverse manufacturing requirements.
- Process-Specific Reactor Design: We develop Chemical Reactors according to capacity, chemical compatibility, operating temperature, pressure, agitation, and heat-transfer requirements.
- Quality Materials & Precision Manufacturing: We use quality-checked materials and advanced fabrication practices to deliver durable, reliable, and low-maintenance reactor systems.
- Automation-Ready Technology: Our reactors can integrate modern sensors, instrumentation, variable-speed drives, and automated controls for accurate and repeatable process operation.
- Reliable Industrial Support: We focus on engineered solutions, consistent manufacturing quality, and application-oriented configurations to support long-term industrial performance.
Suyom Engineering is a leading Chemical Reactor Manufacturers, Suppliers and Exporters in India. We deliver engineered Chemical Reactor solutions focused on controlled reactions, dependable fabrication, efficient thermal management, and scalable industrial performance. Our product approach combines suitable metallurgy, process-specific design, automation readiness, and modern reactor-engineering developments to meet evolving requirements across chemical, pharmaceutical, agrochemical, polymer, and specialty manufacturing industries. Contact us today for more information!
Frequently Asked Questions (FAQs)
You should consider reaction type, capacity, temperature, pressure, chemical compatibility, agitation, and heat-transfer requirements.
Stainless steel such as SS 304 or SS 316/316L is commonly selected based on corrosion resistance and process compatibility.
A 3kL Chemical Reactor is commonly used for medium-scale chemical production requiring controlled mixing, reaction, heating, and cooling.
Yes, Chemical Reactors can incorporate sensors, programmable controls, variable-speed drives, and automated temperature or pressure management.
Chemical, pharmaceutical, agrochemical, polymer, resin, adhesive, specialty chemical, and other process industries use Chemical Reactors.